TLDR
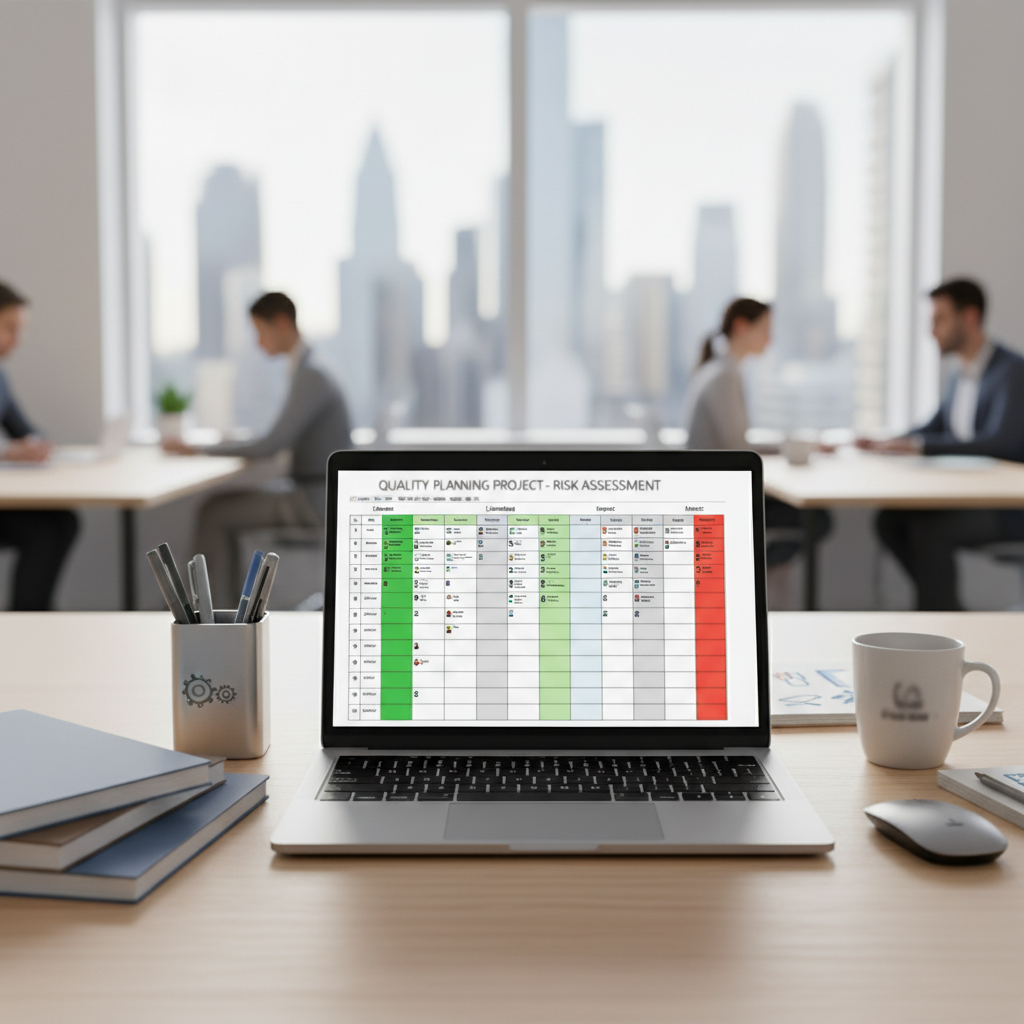
A well-structured FMEA (Failure Mode and Effects Analysis) template is the starting point for effective risk analysis. This post walks through the key columns, scoring criteria, and structure needed for both Design FMEA (DFMEA) and Process FMEA (PFMEA) in the current AIAG-VDA format.
Covers template structure, the 7-step AIAG-VDA approach, severity/occurrence/detection rating scales, Action Priority (AP) ratings, and best practices for filling out your FMEA.
Why You Need a Good FMEA Template
Failure Mode and Effects Analysis (FMEA) is one of the five core quality tools required by IATF 16949 and the AIAG (Automotive Industry Action Group). It is a systematic method for identifying potential failure modes, assessing their risk, and prioritizing actions to prevent them.
A good template enforces the correct structure, prompts the team through every required field, and ensures consistency across programs. A bad template (or no template at all) leads to incomplete analysis, inconsistent scoring, and FMEAs that exist on paper but provide no real value.
The current standard for automotive FMEA is the AIAG-VDA FMEA Handbook, published jointly by AIAG and VDA (Verband der Automobilindustrie) in 2019. This handbook replaced the previous AIAG FMEA manual (4th edition) and introduced significant changes to the format and methodology.
DFMEA vs. PFMEA: Key Differences
Both types of FMEA follow the same methodology, but they analyze different things:
DFMEA (Design FMEA) analyzes the product design. It asks: “How could this design fail, and what would be the consequences?” The focus is on design functions, failure modes related to the design, and design controls (verification and validation activities).
PFMEA (Process FMEA) analyzes the manufacturing process. It asks: “How could this process step fail, and what would be the consequences?” The focus is on process functions, failure modes related to manufacturing, and process controls (prevention and detection methods).
Both types should be linked. Failure modes identified in the DFMEA that cannot be fully addressed through design changes should flow into the PFMEA as process requirements. The control plan is then built from the PFMEA outputs.
The AIAG-VDA 7-Step Approach
The AIAG-VDA FMEA Handbook organizes the analysis into seven steps:
- Planning and Preparation: Define the scope, boundaries, team, and timing of the FMEA.
- Structure Analysis: Break down the system into its components (DFMEA) or the process into its steps (PFMEA). Define the structure tree showing relationships between elements.
- Function Analysis: Identify the function of each element and the requirements it must fulfill.
- Failure Analysis: Identify potential failure modes, effects, and causes. Build the failure chain: cause leads to failure mode leads to effect.
- Risk Analysis: Rate each failure chain for Severity (S), Occurrence (O), and Detection (D). Determine the Action Priority (AP) rating.
- Optimization: Define and implement actions to reduce risk for high-priority items. Re-rate after actions are completed.
- Results Documentation: Document the final FMEA, communicate results, and link outputs to the control plan.
Template Structure: Required Columns
A compliant AIAG-VDA FMEA template should include the following columns (organized by the 7-step approach):
Header Information
- FMEA type (DFMEA or PFMEA)
- Part name and number
- Drawing revision and date
- Team members
- FMEA start date and revision history
- Customer and plant/location
Structure and Function (Steps 2-3)
- Focus Element (the component or process step being analyzed)
- Higher-Level Element (the next-higher assembly or next process step)
- Lower-Level Element (sub-component or process input, such as a machine characteristic)
- Function of the Focus Element
- Requirement associated with the function
Failure Analysis (Step 4)
- Failure Effect (impact on the higher-level element or end user)
- Failure Mode (how the focus element fails to meet its function/requirement)
- Failure Cause (what causes the failure mode at the lower-level element)
Risk Analysis (Step 5)
- Severity (S) rating: 1 to 10
- Current Prevention Controls
- Occurrence (O) rating: 1 to 10
- Current Detection Controls
- Detection (D) rating: 1 to 10
- Action Priority (AP): High, Medium, or Low
Optimization (Step 6)
- Recommended Action
- Responsible Person
- Target Completion Date
- Action Taken
- Completion Date
- Revised S, O, D ratings
- Revised AP rating
Severity, Occurrence, and Detection Rating Scales
The AIAG-VDA Handbook provides detailed rating tables for S, O, and D. Here is a simplified overview:
Severity (S): How serious is the effect?
- 10: Hazardous without warning (safety or regulatory noncompliance)
- 9: Hazardous with warning
- 7-8: Major impact on product function
- 4-6: Moderate impact, reduced performance
- 2-3: Minor impact, noticeable but not significant
- 1: No discernible effect
Occurrence (O): How likely is the cause?
- 10: Extremely high (failure is almost inevitable)
- 7-9: High (frequent failures)
- 4-6: Moderate (occasional failures)
- 2-3: Low (relatively few failures)
- 1: Very low (failure unlikely, strong prevention controls)
Detection (D): How likely is the control to detect the failure?
- 10: No detection method, or detection method is unproven
- 7-9: Low chance of detection
- 4-6: Moderate chance of detection
- 2-3: High chance of detection
- 1: Almost certain detection (automated, error-proof)
Action Priority (AP) vs. RPN
The AIAG-VDA Handbook replaced the Risk Priority Number (RPN = S x O x D) with the Action Priority (AP) system. Instead of a single number from 1 to 1,000, the AP system classifies each failure chain as High, Medium, or Low priority using a lookup table based on the combination of S, O, and D values.
The AP system addresses a long-standing criticism of RPN: that identical RPN numbers could represent very different risk profiles. An RPN of 200 from S=10, O=2, D=10 is very different from S=5, O=5, D=8, but the old system treated them the same.
The AP table ensures that high-severity items always receive attention, regardless of their occurrence and detection ratings.
Best Practices for Completing Your FMEA
- Use a cross-functional team. FMEA is not a solo activity. Include design engineering, manufacturing, quality, maintenance, and anyone with relevant expertise.
- Be specific. “Part is bad” is not a useful failure mode. “Bore diameter undersized by more than 0.05 mm” is.
- Separate prevention from detection. Prevention controls stop the failure from occurring. Detection controls find the failure after it occurs. Do not mix them up.
- Rate honestly. Inflating detection scores or deflating occurrence scores to avoid action items defeats the purpose. The FMEA is only useful if the ratings reflect reality.
- Link to the control plan. Every detection control in the PFMEA should appear in the control plan. If it is not in the control plan, it is not being controlled.
- Keep it alive. An FMEA is a living document. Update it when processes change, when new failure modes are discovered, and when actions are completed.
Frequently Asked Questions
Is the RPN still used?
The AIAG-VDA Handbook replaced RPN with Action Priority (AP). However, some customers and internal systems still use RPN. Check your customer-specific requirements. If your customer has not adopted the AIAG-VDA format, you may still be using the older AIAG 4th edition format with RPN.
Can I use the same template for DFMEA and PFMEA?
Yes. The column structure is the same. The difference is in the content: DFMEA analyzes design functions and design controls, while PFMEA analyzes process functions and process controls. A single workbook with separate tabs for DFMEA and PFMEA is a practical approach.
How detailed should the FMEA be?
Detailed enough to identify all significant risks, but not so detailed that the team gets lost. Focus on the characteristics that affect safety, fit, function, and customer satisfaction. Use the DFMEA/PFMEA scope to set boundaries.
When should the FMEA be started?
DFMEA should begin during Phase 2 (Product Design) of APQP (Advanced Product Quality Planning). PFMEA should begin during Phase 3 (Process Design). Starting the FMEA after the design or process is finalized limits its value because changes are more costly at that point.
Is FMEA software worth it?
For organizations managing many FMEAs or requiring strong linkage between FMEA, control plan, and process flow, dedicated software (Relyence, APIS IQ, Omnex) adds significant value. For smaller operations with fewer products, a well-structured Excel template is sufficient.
What happens during an audit if the FMEA is incomplete?
An incomplete FMEA is a common audit finding. Auditors look for evidence that the FMEA covers all relevant failure modes, that ratings are justified, that actions are tracked to completion, and that the FMEA is linked to the control plan. Gaps in any of these areas can result in a nonconformity.
Stay Current on Automotive Quality
PPAP updates, GD&T guidance, and practical quality resources delivered to your inbox. No spam, just what quality professionals need to know.
Subscribe
Leave a Comment